
Production and Industrial Engineering
GATE PI topic:metal-forming PYQs
Build your understanding with focused practice from past exam papers.
Questions 11–20 of 23. Imported answers require independent review unless marked reviewed.
Question 49
Open questionPINAT2 marksNeeds review
During a hot-working process, the homologous temperature is 0.8. The melting point of the work metal is 800 °C. The temperature (in °C) during hot-working is____________. [round off to nearest integer]
Log in to check the answer
You can attempt this question now. Sign in to view the answer key, explanations and discussion.Log in to check answerQuestion 50
Open questionPINAT2 marksNeeds review
A workpiece of 30 mm diameter and 40 mm height is compressed between two plates in an open die forging process. Assume a perfectly plastic material with a flow stress of 300 MPa. The ideal forging load (in kN) at 30% reduction (in height) is____________. [round off to nearest integer]
Log in to check the answer
You can attempt this question now. Sign in to view the answer key, explanations and discussion.Log in to check answerQuestion 8
Open questionPIMCQ1 markNeeds review
Match the component with the corresponding manufacturing process in the table below.
Component | Manufacturing process |
|---|---|
P: Aluminum alloy piston for IC engine | 1: Blow molding |
Q: Low carbon steel oil pan | 2: Powder metallurgy |
R: Tungsten carbide cutting tool insert | 3: Sand casting |
S: Plastic bottle | 4: Deep drawing |
Your answerChoose one option.
Log in to check the answer
You can attempt this question now. Sign in to view the answer key, explanations and discussion.Log in to check answerQuestion 19
Open questionPINAT1 markNeeds review
A cylindrical mild steel tensile test specimen of gauge length 50 mm and diameter 10 mm is extended in two stages at a deformation speed of 4 mm/min. The specimen is extended from 50 mm to 55 mm in the first stage, and from 55 mm to 60 mm in the second stage. Neglecting elastic deformation, the total longitudinal true strain is ____________. [round off to 2 decimal places]
Log in to check the answer
You can attempt this question now. Sign in to view the answer key, explanations and discussion.Log in to check answerQuestion 43
Open questionPINAT2 marksNeeds review
A wire of 5 mm diameter is drawn into a wire of 4 mm diameter through a conical die at a constant pulling speed of 5 m/s. Neglecting the coefficient of friction and redundant work, the drawing stress (
) in MPa for the above process is given by
, where
is the mean flow strength of wire material in MPa, and
is the ratio of decrease in area of cross-section to initial area of cross-section of the wire. If the mean flow strength of wire material is 600 MPa, then the power required in kW in the above wire drawing process is ________.
[round off to 2 decimal places]Log in to check the answer
You can attempt this question now. Sign in to view the answer key, explanations and discussion.Log in to check answerQuestion 55
Open questionPINAT2 marksNeeds review
A 3.5 mm thick sheet is rolled using a two high rolling mill to reduce the thickness under plane strain condition. Both rolls have a diameter of 500 mm and are rotating at 200 RPM. The coefficient of friction at the sheet and roll interface is 0.08, and the elastic deflection of the rolls is negligible. If the mean flow strength of the sheet material is 400 MPa, then the minimum possible thickness (in mm) of sheet that can be produced in a single pass is ________.
[round off to 2 decimal places]
Log in to check the answer
You can attempt this question now. Sign in to view the answer key, explanations and discussion.Log in to check answerQuestion 44
Open questionPINAT2 marksNeeds review
A cylindrical billet of 90 mm diameter is extruded to produce an I-section as shown in the figure (all dimensions in mm).
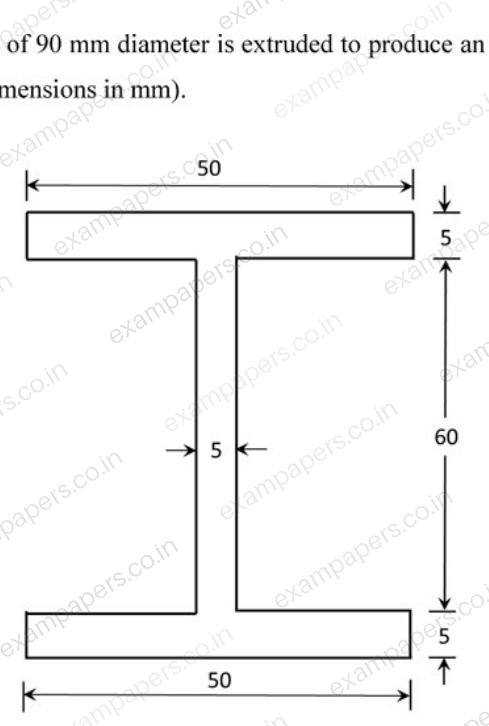
The total extrusion pressure (
) in MPa required for the above process is given by
where,
is the mean flow stress of the material, and
and
are the initial and the final cross-sectional areas, respectively. If the mean flow stress of the extruded material is 80 MPa, the force required for the above extrusion (rounded off to one decimal place) in kN is __________.Log in to check the answer
You can attempt this question now. Sign in to view the answer key, explanations and discussion.Log in to check answerQuestion 10
Open questionPIMCQ1 markNeeds review
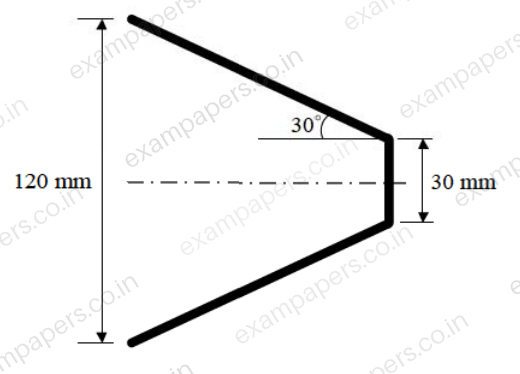
The end product obtained using spinning process is shown in the figure. The initial blank thickness is 2.5 mm. The blank diameter (in mm) is
Your answerChoose one option.
Log in to check the answer
You can attempt this question now. Sign in to view the answer key, explanations and discussion.Log in to check answerQuestion 32
Open questionPIMCQ2 marksNeeds review
A 100 mm long cylindrical workpiece of diameter 50 mm is reduced to 25 mm diameter using extrusion process. The flow curve for the metal has strength coefficient as
MPa and the strain hardening co-efficient is 0.15. Assuming no friction and no redundant work, the required ram pressure (in MPa) is closest toYour answerChoose one option.
Log in to check the answer
You can attempt this question now. Sign in to view the answer key, explanations and discussion.Log in to check answerQuestion 24
Open questionPINAT1 markNeeds review
In a two-pass wire drawing process, there is a 40% reduction in wire cross-sectional area in 1st pass and further 30% reduction in 2nd pass. The overall reduction (in percentage) is ______
Log in to check the answer
You can attempt this question now. Sign in to view the answer key, explanations and discussion.Log in to check answer